


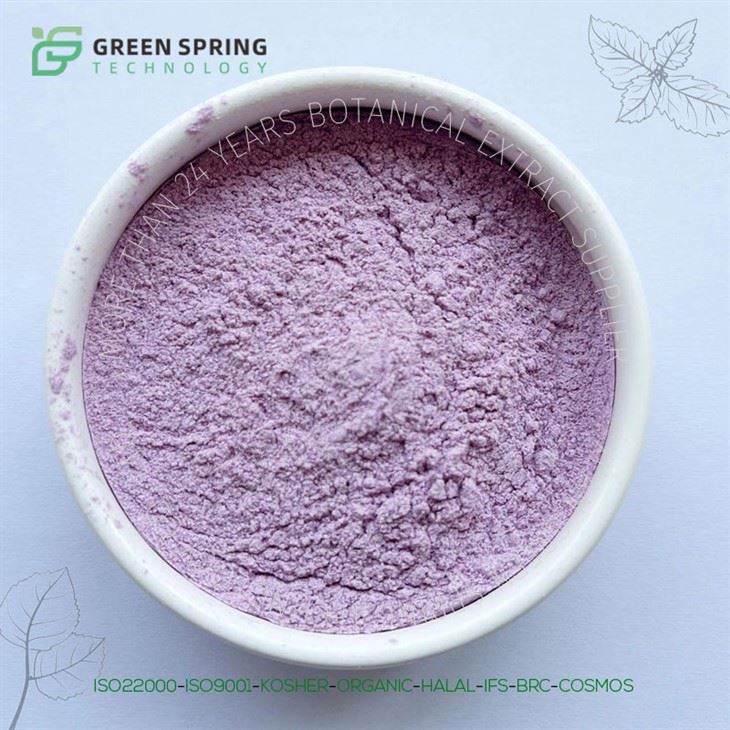

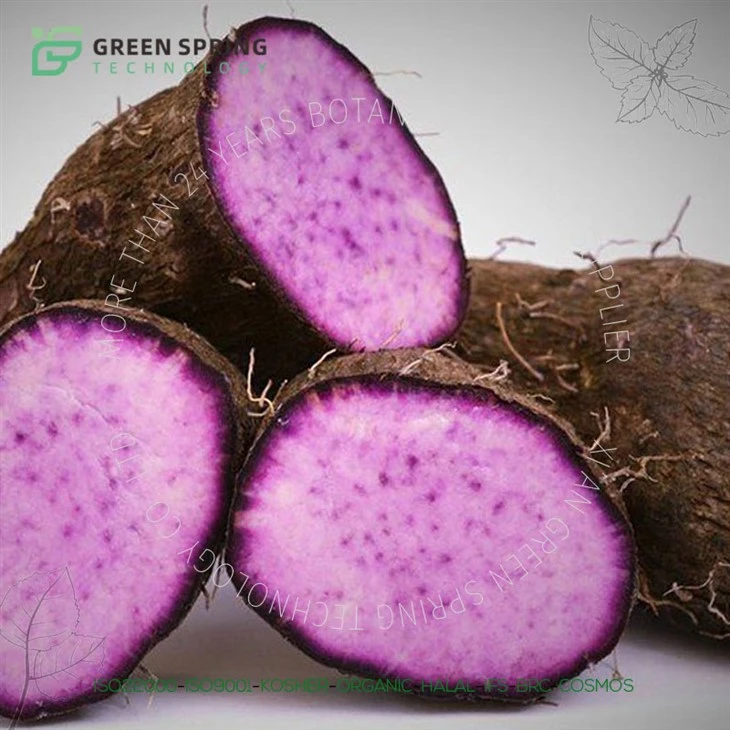
Bulk Premium Natural Ube Powder (Purple Yam)
Dioscorea Alata · 100% Pure Purple Yam · Low-Temperature Processed · Authentic Earthy Sweetness & Vibrant Natural Purple Hue for Food, Beverage & Bakery Manufacturing
R&D Insights: Solving Color Degradation, Texture Inconsistency & Batch Fluctuation in Ube Processing
Why food engineers and commercial bakers trust our specialized low-temperature ube processing technology.
If you have ever formulated with commercial purple sweet potato or low-grade ube powders, you know the common headaches: natural purple colors turning into unappealing brownish-gray during baking or pasteurization, inconsistent starch gelatinization that ruins dough elasticity, or artificial flavorings that leave a synthetic chemical aftertaste.
Our Bulk Natural Ube Powder is crafted strictly from selected premium whole Dioscorea Alata tubers. We utilize a proprietary gentle cooking and low-temperature dehydration technique that locks in both natural anthocyanin antioxidants and delicate nutty, vanilla-like aromatic compounds. The result is an industrial-grade ingredient that offers heat-stable rich purple coloration, uniform starch swelling capacity, rapid hydration, and zero artificial additives-giving your RTD beverages, ice creams, boba mixes, and bakery goods an authentic taste and flawless visual appeal every single batch.
Technical Specifications
| Botanical Source | Dioscorea alata (True Purple Yam / Ube Tubers) |
| Product Grade & Type | 100% Dehydrated Whole Ube Powder / Dehydrated Pre-Gelatinized Ube Flour |
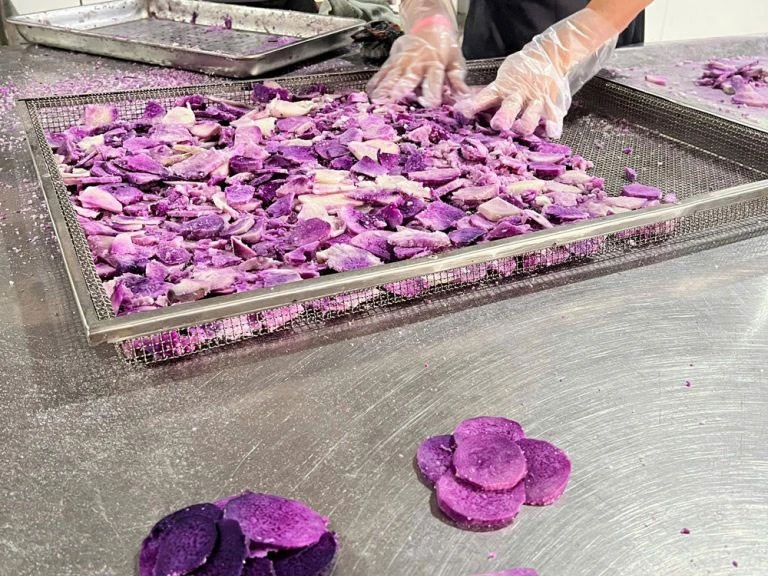
| Processing Method | Steam Cooked & Low-Temperature Dehydration / Fine Air-Milling |
| Appearance & Flavor | Fine vibrant purple to deep violet powder; mild, naturally sweet, nutty vanilla flavor |
| Particle Size / Mesh | 80 – 120 Mesh (Custom ultra-fine mesh available for beverage applications) |
| Moisture Content | ≤ 6.0% (Strictly moisture-controlled for long-term shelf stability) |
| Heavy Metal Limits | Pb < 0.5 ppm | As < 0.5 ppm | Cd < 0.2 ppm | Hg < 0.05 ppm |
| Microbial Control | Total Plate Count < 5,000 cfu/g; Yeast & Mold < 100 cfu/g; E. coli / Salmonella Negative |
| Shelf Life & Storage | 18–24 Months when stored in a cool, dry environment in sealed moisture-proof drums |
Trusted UBE POWDER MANUFACTURER & SUPPLIER



Product Specifications
| Product SKU Code | Grade Nomenclature & Product Type | Specification Metrics | Primary Sourcing Focus |
|---|---|---|---|
| UBE-CONV-100P | Conventional Ube Powder (100% Pure Fruit Base) | 80-120 Mesh / Moisture ≤ 6.0% | Premium commercial standard for industrial baking, food processing, and dynamic corporate formulations. |
| UBE-ORGA-100P | Certified Organic Ube Powder (100% Pure Fruit Base) | 80-120 Mesh / Moisture ≤ 5.0% | Fully audited organic supply chain for premium clean-label brands, high-end nutraceuticals, and organic retail markets. |
📄 Request Official Quality Documents & Test Reports (Free PDF)
Need batch-specific lab results or customs compliance files? We provide official stamped documents for your quality audit:
Standard Specs: COA | TDS | Flow Chart | MSDS / SDS
Quality & Safety: Nutrition Facts | 3rd-Party Test Report | Compliance Cert | Pesticide Residue | Residual Solvent
Request Documents Now → ⚡ Guaranteed reply within 24 hours
One-Stop OEM / ODM Customization & Bulk R&D Supply Chain
We bridge the gap between industrial raw material supply and retail market readiness. In addition to supplying premium Bulk Wholesale Cargo for corporate formula development, food manufacturing, and pilot lab R&D, our facility offers turnkey OEM and ODM private label services. From custom blending modifications to retail-ready premium packaging structures, we match your exact market positioning.
Stand-up Pouch Series (Private Label)
Ideal for retail groceries, fitness brand protein powder additions, and baking mix brands. Features high-barrier airtight closures to secure anthocyanin shelf stability.
- 100g / 300g / 500g Stand-up Pouch
Premium Tin Can Series (Private Label)
Perfect for high-end boutique tea spaces, premium barista lattes, and premium functional gift packaging layouts. Complete light-blocking shield prevents oxidation loops.
- 50g / 100g / 200g Premium Tin Can

Ube Powder application field
Application Track 1: Commercial Baking & Confectionery Coloring Stability
Acts as a robust, natural alternative to artificial violet dyes. The high starch matrix structure of raw Ube protects the natural pigments during standard baking processes, preventing fading into grey tones.
R&D Directives: Deploy "Conventional" or "Certified Organic''grades directly into dry flour weight segments. Highly recommended for commercial bread plants, donut glazing systems, and large-scale pastry processing lines.
Application Track 2: RTD Beverages & Instant Powder Mix Solubility
Delivers clean purple visual aesthetics and traditional sweet nutty notes to beverage systems without introducing gritty residue layers at the bottom of the cup.
R&D Directives: Incorporate our ultra-fine mesh layouts into pre-blended milk powders or instant boba tea mixes. Yields reliable visual stability and rich authentic flavor notes.
Application Track 3: Ultra-Premium Frozen Dairy & Gourmet Clean-Label Food Products
Maintains complete flavor fidelity and deep lavender color performance when suspended in cold dairy fats, completely eliminating the need for added artificial coloring agents.
R&D Directives: Integrate our **Certified Organic Ube Powder** into ice cream pasteurizer lines or fine pastry paste frameworks. Perfect for premium clean-label grocery products targeting eco-conscious demographics.
Product Application Cases
Case Study 1: Resolving Baking Fading Loops in Global Confectionery Lines
Operational Challenge: A multinational snack manufacturer suffered heavy consumer complaints because their premium ube cakes faded into an unappealing grayish-brown hue under industrial tunnel oven temperatures.
The Technical Execution: R&D teams replaced their standard purple yam paste supply with our heat-resilient Philippine Ube powder matrix.
✓ Commercial Outcome: Baked products maintained an authentic, vibrant violet shade with zero artificial dye additions. Product waste dropped by 34% and regional sales expanded rapidly.
Case Study 2: Eradicating Sediment Clumping in Instant Milk Tea Mixes (Melbourne, Australia)
Operational Challenge: An international beverage brand's newly launched ube latte series suffered poor review ratings due to chalky particles and rapid grit precipitation forming at the bottom of customer mugs.
The Technical Execution: Blending lines upgraded their input raw materials to our ultra-fine, cold-soluble superfine powder blend.
✓ Commercial Outcome: Achieved instant, silky-smooth dispersion within liquid bases. Customer re-order performance surged by 58% over consecutive fiscal quarters.
Customer Review
"The color consistency of this ube powder across diverse manufacturing batches is exceptional. It lets us maintain tight corporate brand visual standards across all our bakery retail franchises."
"Our retail consumers demand clean labels. Finding a direct global supplier providing rich purple yam color and authentic flavor profile with absolutely zero filler starches is a game changer."
"This powder blends smoothly into our gourmet ice cream formulations. No aggregation issues, no synthetic smell, just natural creamy ube characteristics that match premium positioning."
Honor and qualification
Official certification, professional after sales service.

USDA ORGANIC

EU ORGANIC

ISO22000

ISO9001

COSMOS

BRC

IFS

FDA

HALAL

KOSHER
Industrial Packaging, Preservation & Supply Chain Logistics
- Standard Bulk Packaging & Custom Label Layouts
Packed inside heavy-duty multi-layer kraft paper drums containing double-layer food-grade polyethylene internal liners (25kg net weight per drum) for large-scale formula developer clients. Retail orders are processed via automated custom private-label stand-up pouches (100g, 300g, 500g) or protective tin cans (50g, 100g, 200g).
- Warehouse Preservation Controls
Store within climate-controlled, dry, dark warehousing spaces kept away from thermal exposures and direct sunlight. Maintain ambient room temperatures strictly below 22°C (71°F) with relative humidity parameters kept under 60%.
- Global Freight & Customs Documentation Manifests
Shipped globally under food-grade dry cargo protocols. Every delivery includes a comprehensive Certificate of Analysis (COA), detailed HPLC color analysis indices, complete microbiological status matrices, organic authenticity tracking papers (for organic SKU), non-GMO certificates, and phytosanitary declarations.
Packaging specifications
Packaging can be customized according to needs

1kg/pack
Packaging size: 32cm (length) x 26cm (width)
Gross weight: 1.07kg
Packaging materials: double-layer food grade PE bag for memory, outer aluminum foil bag

5Kg/aluminum drum
Packaging size: 36cm (height) x 25cm (diameter)
Gross weight: 1.1kg
Packaging material: double-layer food grade PE bag for memory, outer sealed aluminum drum

10Kg/box
Packaging size: 53cm (length) x 30cm (width) x 37cm (height)
Gross weight: 13kg
Packaging materials: double-layer food grade PE bag for memory, sealed aluminum drum on the outer layer, 5Kg/aluminum drum x 2, plus full cardboard box

25Kg/Drum
Packaging size: 62cm (height) x 43cm (diameter)
Gross weight: 28kg
Packaging material: double-layer food grade PE bag for memory, plus an additional layer of black food grade PE bag to avoid light
Frequently Asked Questions (Technical Support & Bulk Procurement)
A: Absolutely not. Our premium ube powder is 100% natural. The vivid purple color profile is derived exclusively from the internal anthocyanin pigments of selected *Dioscorea alata* crops, preserved using optimized low-temperature dehydration sequences.
A: Natural anthocyanins are highly sensitive to pH environments. In standard neutral food and dairy matrices (pH 6.0–7.0), our powder displays its classic deep purple/lavender presentation. In highly acidic environments, it shifts toward reddish profiles, which can be easily managed via minor buffering adjustments.
A: No. Our pure grades are entirely filler-free to suit strict clean-label standards. We rely on deep-dehydration controls to maintain powder fluidity, ensuring that you receive 100% authentic purple yam raw materials.
A: Our factory lines operate under rigorous international quality architectures, including FSSC22000, ISO22000, HACCP systems, certified Organic audits, Halal compliance, and certified Good Manufacturing Practices (GMP).
A: Our bulk wholesale MOQ is 100kg (4 standard drums), while private label packaging MOQ varies by container size. To assist your R&D team with color stability evaluations, viscosity metrics, or flavor diagnostic trials, we provide 200g to 500g factory pilot verification samples along with complete technical documentation manifests.
★ Stabilize Thermal Color Performance, Elevate Visual Premiumization, and Ensure True Clean-Label Sourcing Compliance.
Click Here to Request Free Corporate R&D Pilot Evaluation Samples (200g–500g) & Secure Factory-Direct Wholesale Tiered Pricing LayoutsHot Tags: Ube Powder bulk, Ube Powder manufacturer, Ube Powder supplier, Purple Yam Powder bulk, Dioscorea alata powder, Organic Ube Powder, Food Grade Ube Powder, Clean‑label purple yam powder for bakery beverage, Low‑temperature dehydrated ube powder,Ube Powder, Purple Yam Powder, Dioscorea alata powder, Organic Ube Powder, bulk Ube Powder, Ube Powder manufacturer


